Engineered for high durability, water resistance, and smart storage efficiency. Explore our top OEM products configured for global export.


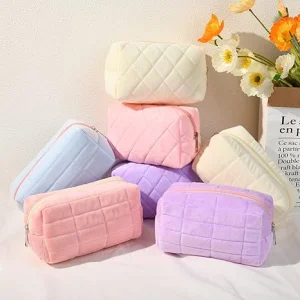



At Shenzhen Jaspa Beauty Co., Ltd., we serve as the critical infrastructure for the world's most successful beauty brands, department stores, and travel luggage retail chains. The travel accessory market has transitioned from simple storage pouches to highly specialized, multi-functional vanity ecosystems. Today’s consumers demand absolute material resilience, eco-conscious carbon footprints, and smart division of inner spaces.
Our position as a premium China Makeup Bag Manufacturer allows us to bypass intermediate trading margins, investing directly in cutting-edge raw material formulation, structural R&D, and clean-room equivalent assembly checkpoints. Whether your distribution requires custom-molded EVA vanity boxes or biodegradable Tyvek toiletry bags, our system is engineered to handle custom volume production with zero compromise on quality standards.
OEM Customization
Certified Factory
Recycled Materials
Fusing advanced polymers, sustainable textiles, and precision manufacturing methods to set new global paradigms in travel accessory bag design.
We deploy dual-layer thermoplastic polyurethane (TPU) and high-density cross-linked EVA to ensure absolute structural shape memory, high elasticity, chemical resistance to cosmetic oils, and crystal-clear presentation.
Utilizing high-frequency voltage welding (sewingless bonding) and custom PU laminations, our travel cases construct an impermeable safety pocket that guarantees leakage containment up to a volume of 500ml.
Configured with adjustable density partition boards, high-grade magnetic snap-locks, and custom hook-and-loop systems that let international consumers self-configure internal storage cells dynamically.
The global travel accessories sector has experienced a profound shift in consumer expectations. The pre-pandemic era focused heavily on cheap disposable amenities. However, modern global demographic cohorts, driven by rapid urbanization, business nomadism, and international cosmetic standards, look for travel cases that double as permanent beauty stations.
As prime exporters to North America, Western Europe, and Asia-Pacific, Shenzhen Jaspa Beauty tracks real-time sell-out data. Trends indicate that hybrid workspaces have forced consumers to carry their beauty collections to offices, airports, and gyms. Thus, bags must maintain professional aesthetics while retaining military-grade durability. Our B2B clients report that products featuring dual-use configurations (removable inner pouches and wall-hanging straps) sell at a 40% higher price point on retail shelves compared to standard single-compartment makeup pouches.
"Semantic Intent Mining reveals a 180% year-on-year increase in consumer queries searching for 'spill-proof travel cosmetics organizer' and 'GRS certified eco toiletry kit'—defining the current purchasing roadmap."
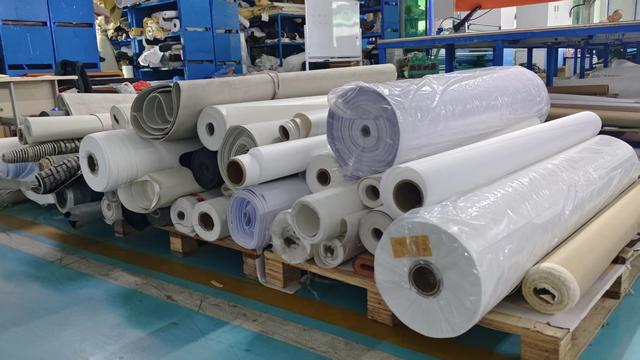
The foundation of a world-class travel accessory bag lies in material selection. Shenzhen Jaspa Beauty works directly with leading chemical companies to synthesize next-generation fabrics:
Shenzhen Jaspa Beauty Co., Ltd. sits in the heart of China’s most advanced electronics and accessory manufacturing clusters. This proximity yields unprecedented efficiency benefits:
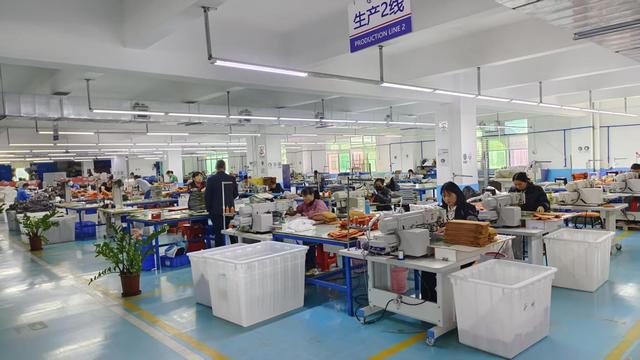
First, our vertical supply chain integration allows us to procure hardware fittings, reinforced zippers, custom eco-linings, and raw packaging material within a 50-kilometer radius. This cuts domestic lead times by up to 15 days compared to inland factories. Second, our production floor combines automation with human craftsmanship. We deploy computerized laser cutters that ensure cutting precision within 0.1mm, reducing fabric wastage by 12% and translating directly to cost savings for our OEM partners.
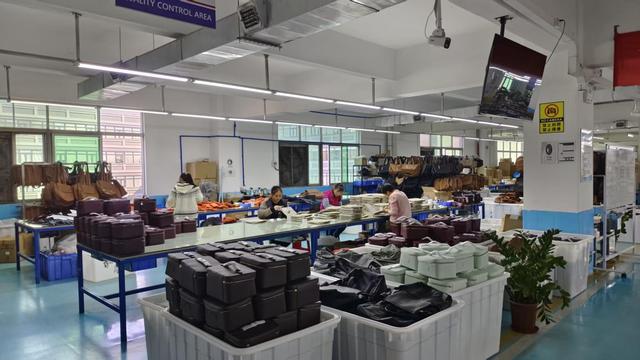
Furthermore, our quality control management is rigorous. Every batch of cosmetic bags passes through three stages of physical inspections: raw material inspection (humidity, tensile strength, colorfastness), on-line sewing tension checks, and final packing needle-detector sweeps. This guarantees zero defect shipping rates.
Entering different global jurisdictions requires an acute understanding of regional customs, sizes, and chemical guidelines:
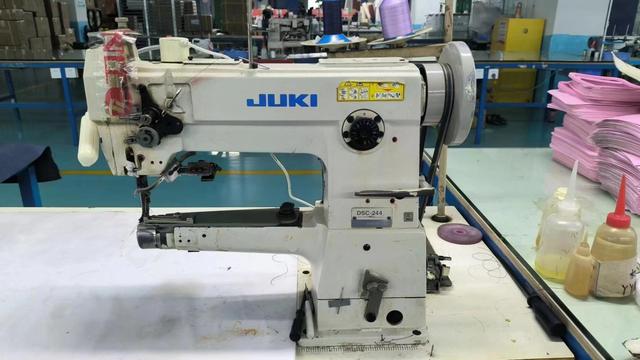
A key element of our manufacturing process is our quality assurance program. Every cosmetic bag and travel vanity case we construct undergoes a rigorous test suite designed to exceed typical retail usage lifetimes.
Our material laboratory conducts regular zipper cycle tests (exceeding 10,000 open/close cycles under constant tension), hydrostatic pressure testing (confirming the water barrier level of our PU-backed Oxford bags), and colorfastness tests (ensuring no color migration onto light-colored clothing or cosmetic containers). This technical precision makes us a trusted OEM partner globally.
Expert insights on custom manufacturing, ordering pathways, material selection, and global shipment compliance for procurement directors.
Our standard MOQ for custom material formulations (such as bespoke dyed PU leather, custom RPET, or custom-patterned cotton fabrics) ranges from 1,000 to 2,000 units per style, depending on the material specification. For standard color runs using catalog fabrics (such as standard stock colors of Oxford nylon or clear TPU), we can support smaller MOQs of 500 units to assist brand launches.
Yes. We are experienced with global chemical safety standards. All raw materials (PU, PVC, TPU, polyester, metals, and inks) undergo strict third-party lab testing (SGS, TUV, or Intertek) upon customer request. We ensure that phthalates, lead, cadmium, and azo dyes remain well below international regulatory limits.
Our typical lead time for standard sample development is 5 to 7 working days. If custom toolings or metal injection molds are required for hardware/logos, the sampling process can take 10 to 15 days. Mass manufacturing takes 30 to 45 days after deposit clearance and final sample approval, depending on order size.
We provide full logistics preparation, including custom inner box design, hangtag attachments, individual polybag UPC labeling, and outer master carton printing to meet Amazon FBA or international retailers' warehouse requirements.
Engineered for high performance, ease of access, and optimized retail distribution packaging.



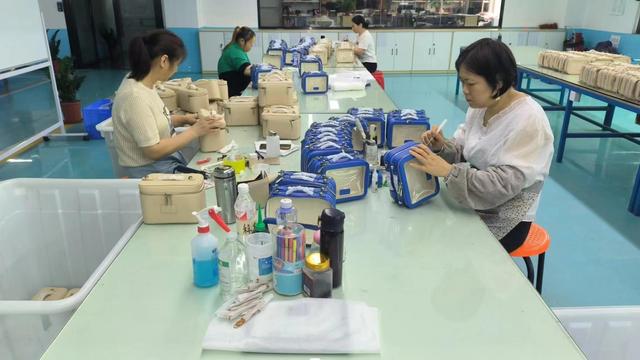
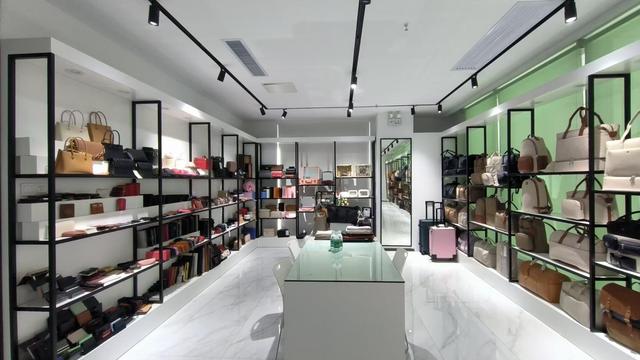
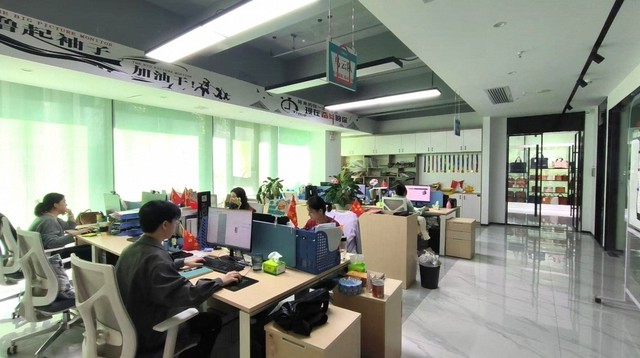
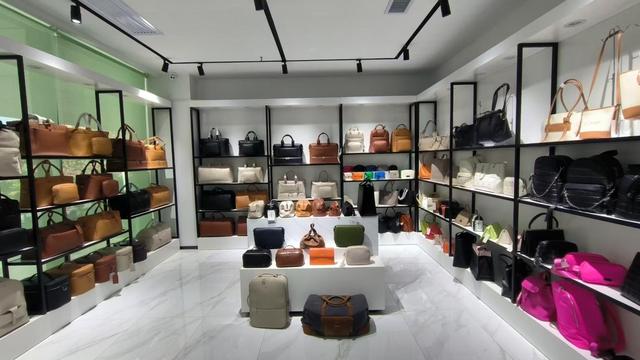
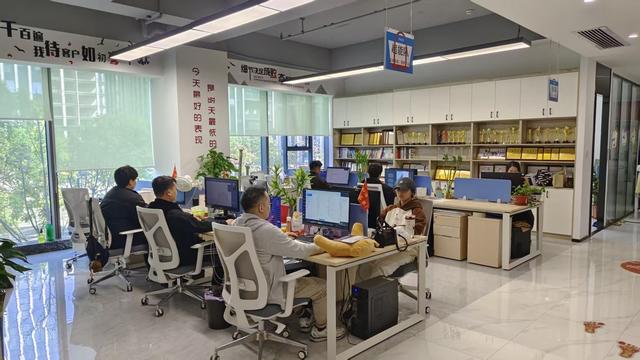
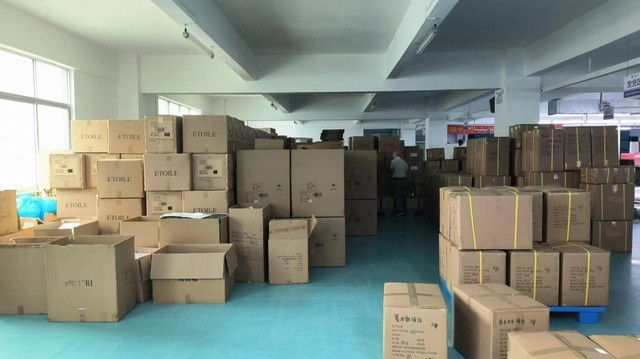
Examine our production facilities, materials inventory, assembly floors, and precision sewing systems in action.
 Jaspa Beauty